Industry application
Home Appliance Sheet Metal Parts and ODM Manufacturing
Panels, brackets and internal structural parts for appliance manufacturers, produced for volume consistency rather than one good sample.
Home appliance parts: the two decisions we focus on
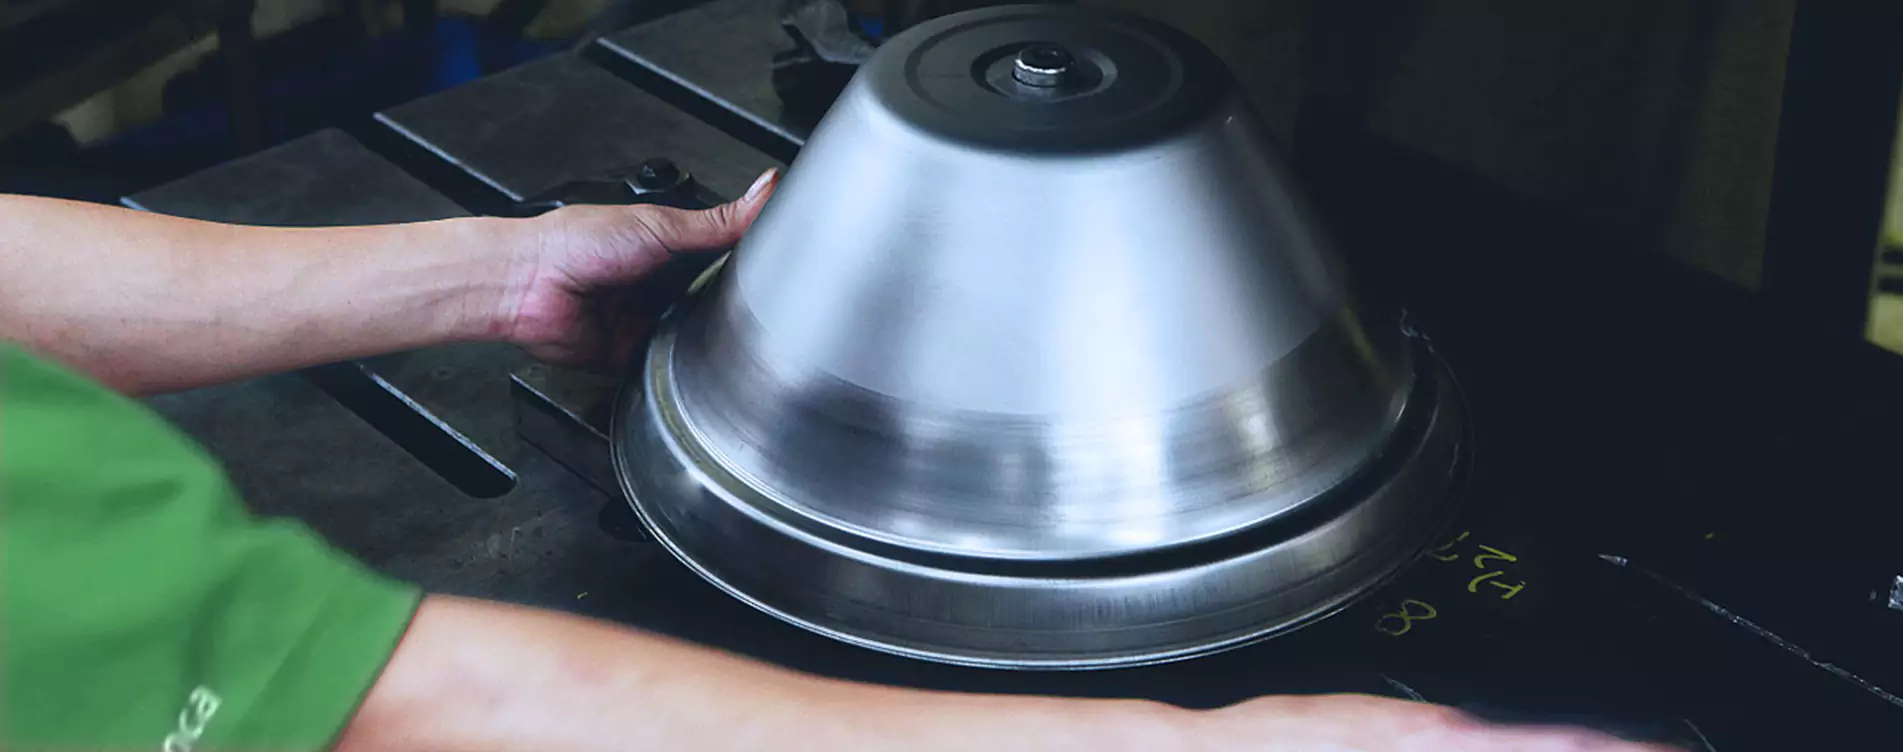
Cost at volume and consistency across a long run, in that order. An appliance part is typically specified once and then produced for years, so the decision that matters most is made before the first piece: whether the part is stamped on a dedicated die or laser cut and formed. Stamping carries tooling cost and returns a low piece price with high repeatability; laser and brake work avoids tooling but costs more per piece and introduces more setup-to-setup variation. Above a few thousand pieces a year, the die usually wins on both cost and consistency. The second consideration is the supplier's ability to hold the same dimension in month thirty as in month one, which comes down to die maintenance and in-process inspection rather than to the original sample. YBT has run one appliance programme of this kind since 2014: electric heaters for a single brand owner at about 20,000 units a year, still in production.
What you check first, and how we handle it
| Criterion | Why it matters here | Where we answer it |
|---|---|---|
| Piece price at volume | The part is produced for years, so unit cost compounds | Stamping |
| Consistency over a long run | Month thirty must match month one | Dies maintained by YBT’s own toolmakers; stamped features inspected to ±0.05 mm during the run |
| Tooling investment decision | Stamping versus laser and brake changes both cost and variation | Customer-paid tooling belongs to the customer; guideline 1,000 pcs without tooling, above 1,000 pcs with tooling |
| Material cost control | Grade and thickness selection drive most of the cost | SPCC, SECC, SGCC and SPHC steels, aluminium and stainless; see the materials guide |
| Capacity headroom | Appliance programmes ramp; the supplier has to absorb it | About 20,000 small parts, 5,000 assemblies and 3,000 finished units a month, indicative |
The processes we use for parts in this sector
Questions you may have about this sector
At what volume does a stamping die pay back?
How do you maintain dimensional consistency over years of production?
What monthly volume can you absorb?
Send an enquiry for this sector
Mention the sector in your message so the reply is framed against the criteria above.
Send us your concept or your drawing
Two separate forms, so you are only asked for what applies to your project.